Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
 author

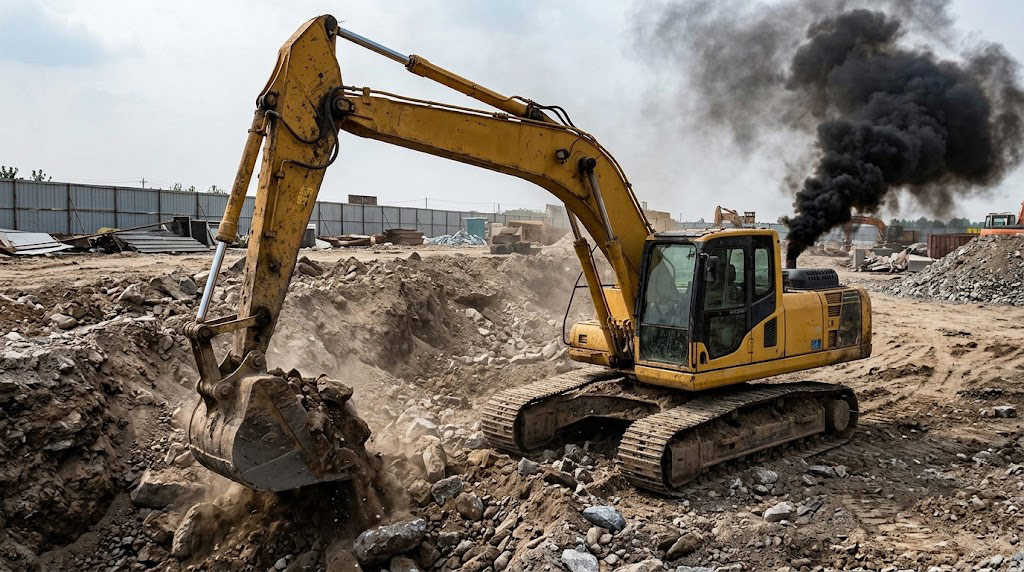
A final drive rarely goes from healthy to completely useless in one instant. More often, the warning period is easy to miss: a new rumble appears during a turn, the housing feels hotter than the opposite side, gear oil starts to seep, or the machine needs more time to climb a familiar grade. Those details matter because a damaged travel gearbox can eventually stop the sprocket while the hydraulic motor is still receiving oil.
The useful response is not to order a complete unit after one unusual sound. Final drive failure symptoms should be compared with the travel motor, brake circuit, hydraulic supply, track tension, and undercarriage. The goal is to catch a mechanical problem early, identify its boundary, and decide whether a gearbox, motor, or complete final drive is the right replacement scope.
The first clues are usually changes from the machine’s normal pattern. Record when the symptom occurs, whether it is present in both travel directions, and whether it becomes clearer after the oil warms. A brief noise on a cold start has a different meaning from a steady mechanical rumble that grows under load.
Excavator final drive noise deserves attention when it follows sprocket speed or becomes louder while turning, climbing, or counter-rotating one track. Grinding, rumbling, clicking, or a repeated knocking tone can point toward gear mesh, bearings, a carrier, or a loose output-side component. Noise by itself cannot identify the failed part. A travel motor, brake, track roller, or packed material can create a similar complaint.
A final drive oil leak is more than a cosmetic issue. Low lubricant level increases contact stress and heat, while a damaged floating seal or shaft seal can let contamination move in as oil moves out. During a planned inspection, note the leak location, oil level, smell, color, and any metallic debris. Fine paste on a magnetic drain plug is not the same evidence as visible chips, but either finding deserves a closer look before the machine returns to production.
A weak travel function does not automatically mean the final drive has failed. The travel motor supplies rotary input; the reduction gears turn that input into usable sprocket torque. If the motor loses displacement, the brake does not release fully, or the valve circuit cannot supply the required flow, the track may slow even when the gearbox is healthy. The pattern below helps separate a warning from a conclusion.
A machine that travels normally on level ground but slows sharply on a slope or while turning may be losing torque, adding mechanical drag, or both. Compare left and right travel under similar engine speed, oil temperature, and ground conditions. If the affected housing also becomes hot or noisy, the reduction unit moves higher on the inspection list. If both tracks weaken together, start farther upstream with pump output, valve flow, relief operation, and oil condition.
Infrared readings or a careful side-to-side comparison can reveal a useful difference, but temperature should be treated as evidence rather than a pass/fail limit. Heat may come from gear friction, bearing damage, brake drag, internal motor leakage, restricted case drain, or an undercarriage that is resisting movement. Check the cause of the heat before approving an excavator travel gearbox failure claim.
A disciplined diagnosis follows the power path. Start with the operator’s command and pilot signal, then check the travel valve section, pump supply, motor inlet and return conditions, brake release circuit, and finally the mechanical output. Use the machine-specific test ports and limits. Generic pressure values are not safe substitutes for the correct service procedure, especially across different excavator families.
Compare both travel circuits at the same engine speed and oil temperature. A pressure drop or inadequate flow on only one side can lead to a valve section, hose restriction, pilot issue, or motor problem. If the hydraulic readings are credible but the affected side still shows grinding, output play, abnormal gear oil, or a hot housing, inspect the final drive mechanically. A sound pump reading does not clear the motor or gearbox, and a noisy gearbox does not prove the pump is at fault.

With the machine secured under the approved maintenance procedure, inspect sprocket fasteners, tooth condition, output play, housing cracks, seal areas, and gear-oil condition. Look for a mismatch between the shaft rotation and sprocket response. A loose sprocket or damaged track component can imitate gearbox failure, while a worn carrier can create play before the drive loses all movement. Keep the hydraulic test record separate from the mechanical inspection record so the replacement decision is based on both.
Production pressure often keeps a machine working after the first warning. That is risky when the noise is rising, the oil level is falling, metal is present, or the housing becomes much hotter than its mate. Continued travel can turn a seal or bearing repair into gear, carrier, and housing damage. It can also spread metal through a connected travel motor or contaminate oil that should have been retained in the circuit.
The stop decision should be tied to evidence: rapid change, visible debris, loss of lubricant, severe vibration, repeated lock-up, or a sprocket that no longer responds smoothly. Isolate the machine, document the operating condition, and preserve the removed oil and filter evidence where practical. A clear record helps a supplier distinguish a component inspection from an urgent complete-unit request.
Final drive replacement is not one universal purchase. A motor-only order would be appropriate if the reduction gears, bearings, output hub, seals, and sprocket interface are serviceable. A gearbox-only repair is sufficient if the hydraulic motor and brake test OK, but the carrier, bearings, or gear set is damaged. In the case of several parts affected by contamination exposure, or when requiring one matched unit with a defined supply boundary, a complete assembly is more appropriate.
It separates walking motors, walking gearboxes, and travel final-drive assemblies rather than treating them as interchangeable names. It lists 21N-27-00190 as a PC1250-8 walking gearbox reference, 708-8H-00440 as a PC300-8M0 travel final-drive assembly reference, and 21T-27-00410 as a PC2000-8 travel gearbox reference. These identifiers help frame the enquiry, but the original tag, serial range, ports, mounting dimensions, brake arrangement, sprocket interface, and requested assembly boundary still need confirmation. Other hydraulic pump models include PC70 hydraulic pump, PC130-7, PC60-7, D475, WA900-3, FD40, D39PX, PC600-7, PC850-8, PC2000-8, PW98, etc.
The 21N-27-00190 travel gearbox is therefore a model-specific lead, not a universal substitute for every PC1250 unit. The same caution applies to the 708-8H-00440 final-drive assembly and the 21T-27-00410 travel gearbox. Send clear photographs of the nameplate and both mounting faces. State whether the quotation should cover the motor, brake, reduction gearbox, output hub, or complete travel device.
A useful request includes the machine model and serial number, original part number, side of the machine, symptom history, cold and hot behavior, oil findings, test readings, photos, and the exact scope required. Ask whether the proposed unit is new, remanufactured, motor-only, gearbox-only, or complete. Ask what has been tested and what remains to be confirmed. Those questions reduce the chance of receiving a component that fits the name but not the machine.
YIKAN KOMSU‘s project materials describe more than two decades of hydraulic maintenance, over 10,000 repair cases, and a 3,000-square-meter automated factory covering casting, CNC machining, heat treatment, assembly, and testing. It also cites CNC precision around +/-0.003 mm, a 99.8% pass rate, one-unit procurement, drawing or sample customization, and technical support for international buyers. Those capabilities matter when a final drive enquiry involves inspection, machining, or a mixed motor-and-gearbox problem rather than a simple catalogue match. The travel and final-drive can help define the component family, while YIKAN KOMSU hydraulic parts give a wider starting point for the enquiry. YIKAN KOMSU produces locally manufactured alternatives for commonly used Komatsu hydraulic components. For fitment confirmation, contact the sales team with the original tag and test record. Continue reading our other guide.
Q1: Is a loud travel drive always a final drive failure?
A1: No. A travel motor, brake, track roller, sprocket, low oil level, or contaminated circuit can create similar noise. Compare hydraulic readings, gear oil condition, output play, and housing temperature before ordering a complete unit.
Q2: Can a final drive oil leak stop a track immediately?
A2: It can, but many leaks first reduce lubrication and increase heat over time. The leak location, oil level, contamination, and gear condition should be checked promptly. Continued travel with low lubricant can turn a seal problem into internal gear damage.
Q3: When is complete final drive replacement justified?
A3: It is more defensible when the gearbox has internal damage, output play, severe contamination, or several failed interfaces, or when the motor and gearbox cannot be separated reliably. The original part number and assembly boundary still need confirmation.